The Complete Guide to Servo Press Brakes: Working Principles, Advantages, Cost Analysis, and Selection Guide
- Share
- publisher
- Daisy Li
- Issue Time
- Oct 21,2026
Summary
Discover how servo press brakes are revolutionizing modern sheet metal fabrication. This comprehensive 2026 guide explores the core differences between all-electric servo and traditional hydraulic systems, featuring deep-dive technical insights into energy savings (up to 70%), micron-level precision (+/- 0.005 mm), full Total Cost of Ownership (TCO) ROI analysis, and an engineering selection roadmap for smart metal workshops.
The Complete Guide to Servo Press Brakes: Working Principles, Advantages, Cost Analysis, and Selection Guide
1. Executive Summary & Industry Paradigm Shift
In precision sheet metal fabrication, precision, cycle speed, energy efficiency, and environmental sustainability define modern competitive advantage. For decades, traditional hydraulic press brakes were the workhorses of metal forming workshops. However, escalating electricity costs, stringent carbon-neutrality mandates, tight tolerance requirements (+/- 0.005 mm / +/- 0.2 deg), and the rising demand for flexible high-mix low-volume (HMLV) manufacturing have exposed the inherent limitations of conventional hydraulic systems.
The Servo Press Brake—particularly the All-Electric Servo Press Brake and the Electro-Hydraulic Servo Hybrid Press Brake—represents the most significant technological leap in bending technology over the past two decades. By replacing or optimizing power-hungry hydraulic pumps with high-torque AC servo motors, precision planetary roller screws, and closed-loop optical encoder feedback, servo press brakes achieve unprecedented bending accuracy, cut power consumption by up to 50% to 70%, eliminate hydraulic oil degradation risks, and slash cycle times by 30% or more.
This comprehensive guide delivers an in-depth technical analysis of servo press brake engineering, comparative performance metrics against hydraulic systems, a rigorous Total Cost of Ownership (TCO) calculation model, and practical selection guidelines for manufacturing professionals worldwide.
2. What is a Servo Press Brake? Working Principles & Architecture
2.1 Core Working Principle
At its fundamental level, a press brake forms sheet metal by driving a punch (upper tooling) into a V-shaped die (lower tooling). While traditional machines rely on continuous hydraulic oil pressurization regulated by proportional valves, an all-electric servo press brake utilizes direct electromechanical servo transmission.
When the operator initiates a bending cycle:
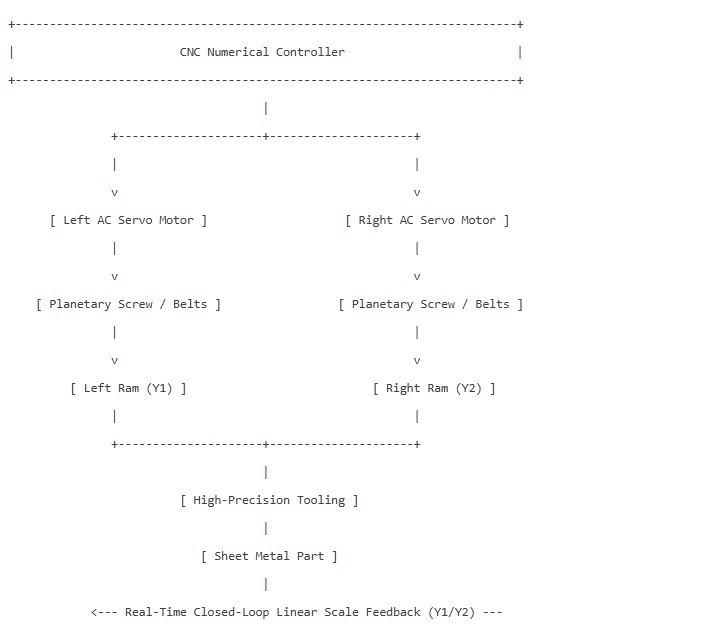
1. The CNC numerical controller calculates the exact stroke depth (Y1/Y2 axes positioning) based on material thickness, tensile strength, V-die opening width, and programmed bending angle.
2. Dual synchronized AC brushless servo motors deliver direct, instantaneous torque to heavy-duty ball screws, planetary roller screws, or high-tensile belt-pulley pulley clusters.
3. The rotational motion of the servo motors is converted into linear downward motion of the upper ram (or upward motion of the lower bed) with micrometer-level precision.
4. Optical linear scales mounted on independent C-frames measure the real-time position of the ram, feeding data back to the CNC at kHz frequencies to ensure closed-loop synchronization between the left (Y1) and right (Y2) cylinders.
2.2 Mechanical Architectures: All-Electric vs. Electro-Hydraulic Hybrid
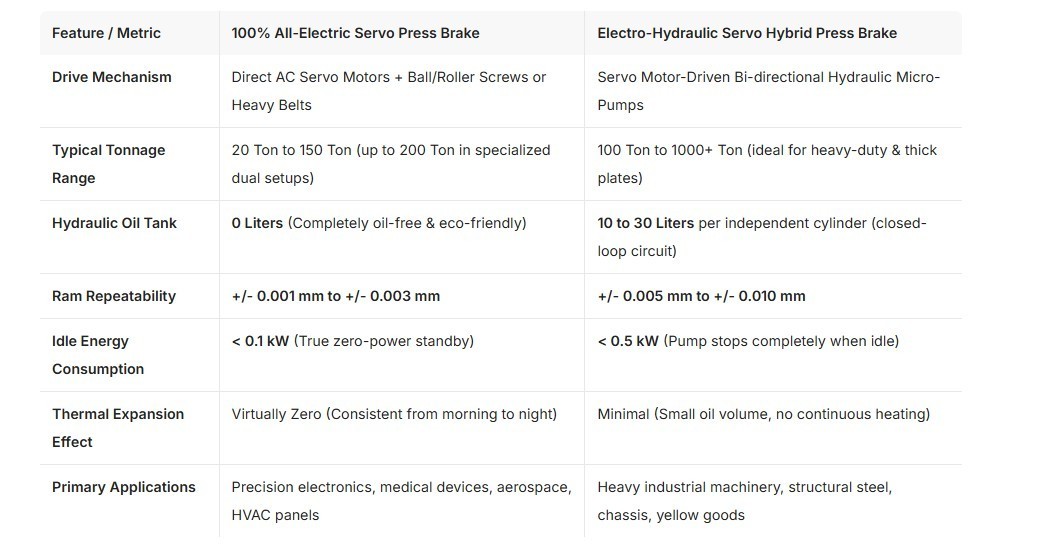
Depending on tonnage requirements and structural design, servo bending technology falls into two primary categories:
3. Servo Electric vs. Traditional Hydraulic: Direct Head-to-Head Comparison
3.1 Energy Efficiency and Power Consumption (50%–70% Savings)
The single greatest operational difference between hydraulic and servo press brakes lies in their power-on profile:
Traditional Hydraulic Press Brake:
●The main asynchronous AC motor runs continuously at full speed (typically 7.5 kW to 37 kW) from the moment the machine is powered on, regardless of whether the operator is bending, loading parts, inspecting angles, or changing tools. Energy is continuously dissipated as heat into the hydraulic oil reservoir.
Servo Press Brake:
●The servo motors consume electricity
only during active motion
. When the ram is stationary, holding a sheet, or in standby mode between bends, electrical draw drops to near zero (< 5% of rated power). During the deceleration and upward return stroke, modern regenerative servo drives can even recover kinetic energy back into the electrical grid or capacitor banks.
3.2 Bending Precision and Thermal Stability
In standard hydraulic machines, hydraulic oil temperature increases from 20 deg C in the morning to 55 deg C after continuous afternoon operation. Because oil viscosity changes with temperature, valve response times drift, causing the ram's bottom dead center (BDC) to fluctuate throughout the working day by as much as 0.05 mm to 0.1 mm—leading to inconsistent bending angles.
Servo electric press brakes eliminate hydraulic thermal drift completely. Equipped with linear encoders with 0.001 mm resolution, the direct mechanical transmission ensures that the first bend produced at 8:00 AM matches the 10,000th bend produced at 10:00 PM down to fractions of a degree.
3.3 Speed and Throughput Enhancement
Servo press brakes deliver superior acceleration and deceleration profiles:
●Approach Speed:Up to 200 mm/s to 220 mm/s (vs. 100–120 mm/s for hydraulic).
●Working Bending Speed:10 mm/s to 25 mm/s with stepless programmable speed modulation.
●Return Speed:Up to 200 mm/s, dramatically shortening idle cycle times.
In high-mix precision production with 4 to 8 bends per workpiece, a servo press brake typically delivers a 30% to 45% increase in daily parts throughput.
3.4 Acoustic Footprint and Environmental Cleanliness
●Noise Level:Traditional hydraulic units generate constant 75 dB(A) to 85 dB(A) pump noise. All-electric servo press brakes operate at under 62 dB(A), creating an ergonomic, whisper-quiet workshop environment.
●Zero Oil Leakage:Eliminating 150 to 400 liters of hydraulic oil avoids periodic oil replacement, filter disposal, sealing ring blowouts, and valve contamination. This makes all-electric servo machines indispensable for cleanroom environments such as medical equipment, pharmaceutical casings, and food-grade stainless steel fabrication.
4. Key Technological Innovations in Modern Servo Press Brakes
Modern servo press brakes are sophisticated cyber-physical systems integrated with advanced sensor technology and smart software algorithms:
4.1 Real-Time Dynamic Crowning & Deflection Compensation
When applying high tonnage across a 2-meter or 3-meter bed, both the upper ram and lower bed naturally experience micro-deflection, which traditionally causes "canoe-shaped" bending defects (over-bent ends and under-bent centers).Modern servo press brakes utilize CNC motorized mechanical crowning systems driven by dedicated servo motors, or multi-point hydraulic wedge matrices that automatically adjust the lower table curve in real-time based on calculated bending tonnage, workpiece length, and material elasticity.
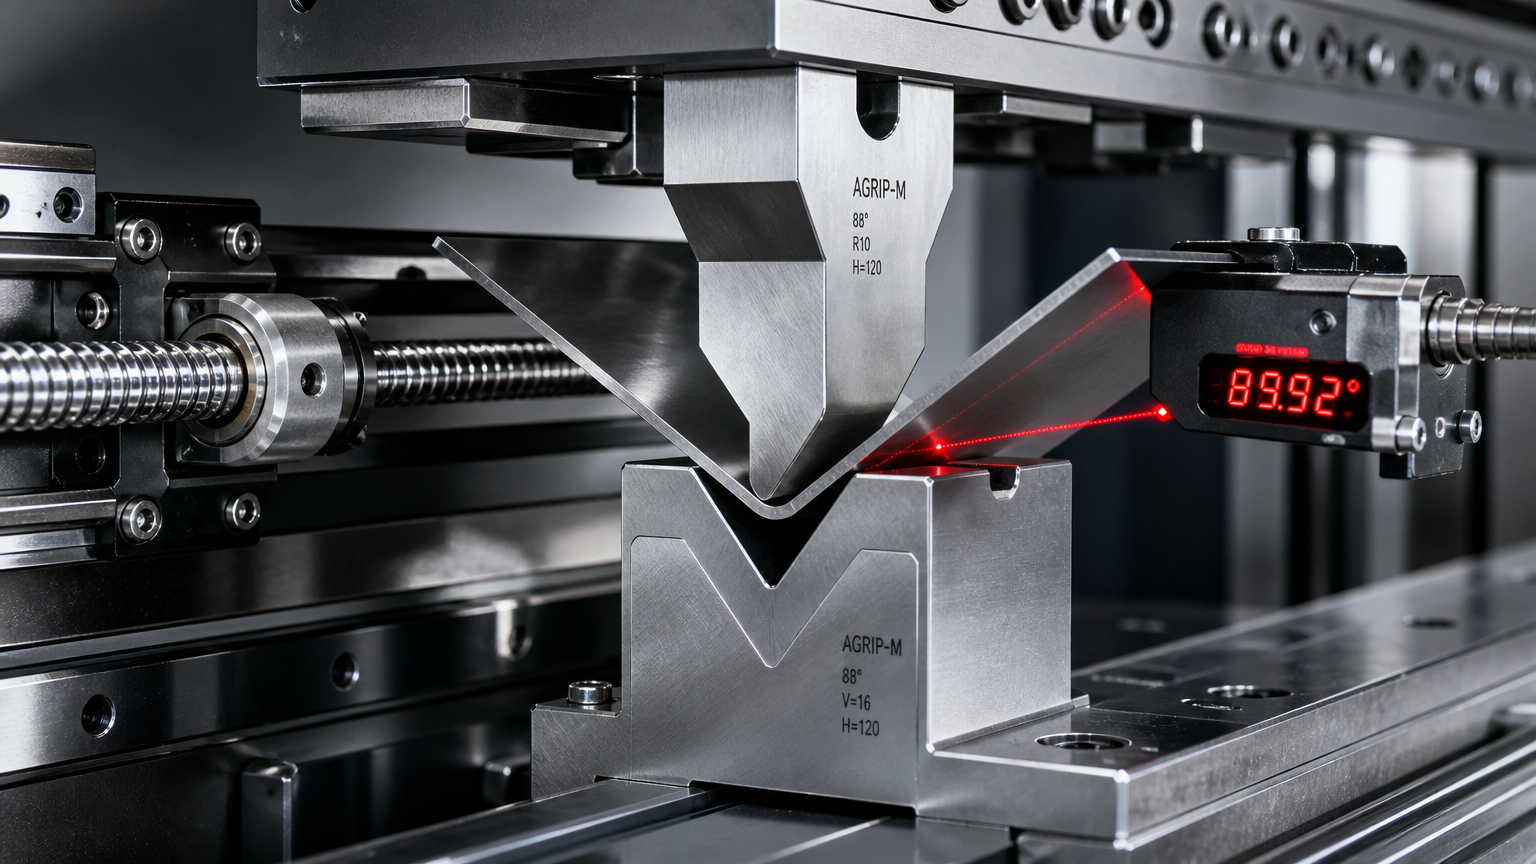
4.2 Integrated Laser Angle Measurement & Adaptive Springback Correction
Material sheet thickness tolerances and rolling direction variances inevitably introduce angle fluctuations. Leading servo press brakes integrate non-contact laser optical angle measurement heads that scan the bending angle in real time during the stroke. If the detected angle deviates from the target (e.g., 90.0 deg), the CNC controller dynamically computes the material's instant springback coefficient and applies micro-correction before the punch releases, guaranteeing first-part accuracy with zero scrap.
4.3 Multi-Axis High-Speed CNC Backgauge Systems
To support rapid bending sequences, servo press brakes are outfitted with 4-axis, 5-axis, or 6-axis (X, R, Z1, Z2, X1, X2) backgauges powered by high-speed servo motors and precision linear guideways. Backgauge positioning speeds exceed 500 mm/s with positioning accuracy within +/- 0.02 mm, enabling seamless processing of complex stepped, tapered, or asymmetrical parts.
4.4 Smart Industry 4.0 & IoT Connectivity
Equipped with open industrial communication protocols (OPC UA, MQTT, EtherCAT), modern servo machines seamlessly communicate with Manufacturing Execution Systems (MES). Plant operators can monitor real-time energy consumption, stroke count, tool wear status, OEE (Overall Equipment Effectiveness), and schedule predictive maintenance before mechanical failures occur.
5. Total Cost of Ownership (TCO) & ROI Economic Analysis
While a servo electric press brake typically commands a 15% to 30% higher initial capital cost (CapEx) than a basic hydraulic machine of equivalent tonnage, its operational expenditure (OpEx) savings deliver rapid payback.
5.1 Real-World Economic Calculation Model
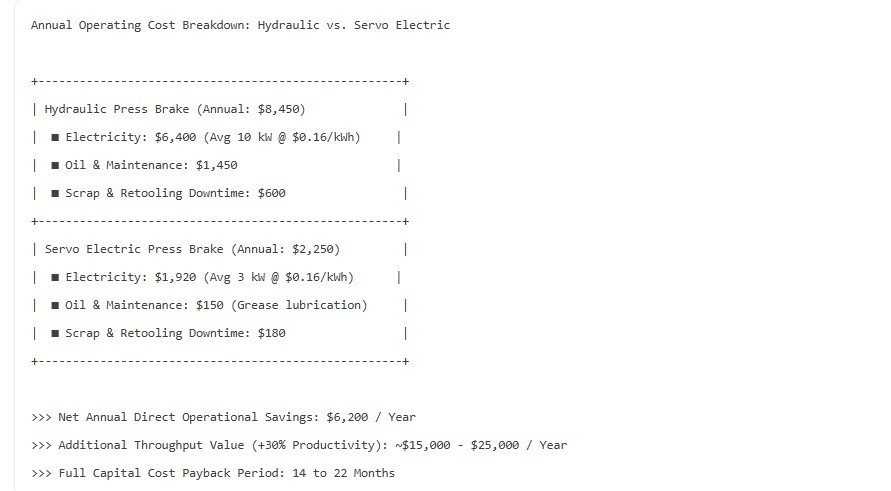
Let us examine a standard manufacturing scenario for a 60-Ton, 2000 mm press brake operating on a two-shift schedule (4,000 operational hours per year):
5.2 Direct Operational Savings Drivers:
1.Electricity Reduction: Consumes electricity only during active bending (3.0 kW average vs. 10.0 kW average load), saving ~$4,480 annually.
2.Maintenance & Fluid Elimination:Zero hydraulic oil purchases ($600/change), zero filter replacements, and zero seal kit overhauls.
3.Scrap Rate Reduction:Real-time angle control reduces test-bend scrap by 70%, saving valuable sheet metal stock (especially on stainless steel, aluminum, and copper alloys).
4.Tooling Longevity: Smooth, shock-free servo deceleration protects delicate hardened punch tips and V-die shoulders from hydraulic pressure spikes.
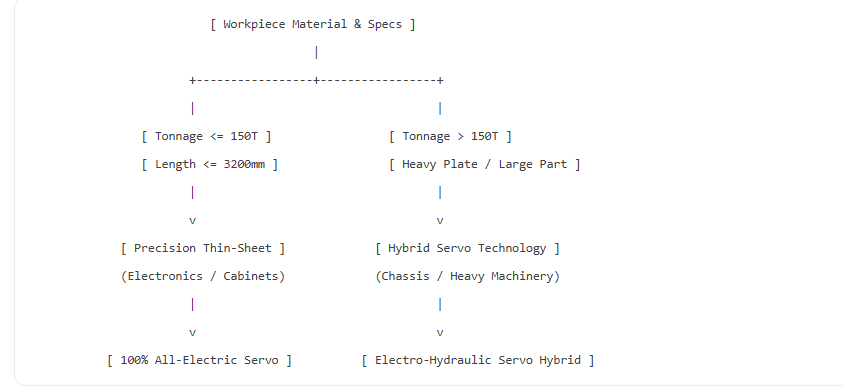
6. Engineering Selection Guide: Choosing the Right Servo Press Brake
Selecting the ideal machine requires balancing workpiece specifications, production batch sizes, and budget constraints:
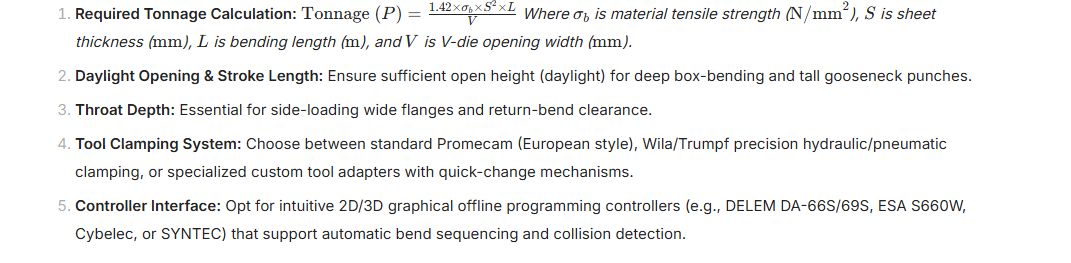
6.1 Essential Technical Parameters Checklist
7. Operational Best Practices & Preventative Maintenance
To maximize accuracy and equipment lifespan over 10+ years of operation:
●Automated Centralized Lubrication:Ensure ball screws and linear guideways receive metered high-grade synthetic grease at programmed stroke intervals.
●Tooling Inspection & Alignment:Regularly verify upper-punch and lower-die centering to prevent asymmetric side-loading on servo mechanical drives.
●Environmental Management:Maintain electrical cabinet dust filters, ensuring cooling fans function properly to protect servo drives and CNC hardware from shop metal dust.
●Periodic Scale Calibration:Clean optical linear glass scales and check reading head air-purge pressure every 6 months to prevent micro-contamination.
8. Conclusion & The Future of Automated Bending
The servo press brake is no longer a luxury niche machine—it is the foundational cornerstone of the modern, automated, and sustainable smart sheet metal factory. As labor markets tighten and energy prices fluctuate, the convergence of all-electric servo mechanics, robotic bending automation (robotic bending cells), and AI-driven adaptive angle compensation will continue to drive fabrication profitability.
For fabricators looking to elevate their manufacturing capabilities, investing in servo press brake technology delivers the ultimate trifecta: uncompromised precision, unmatched speed, and industry-leading energy efficiency.